Burst Factor Improvement: How a Cationic Wet-End Polymer Lifts BF by 15% and Cuts Starch
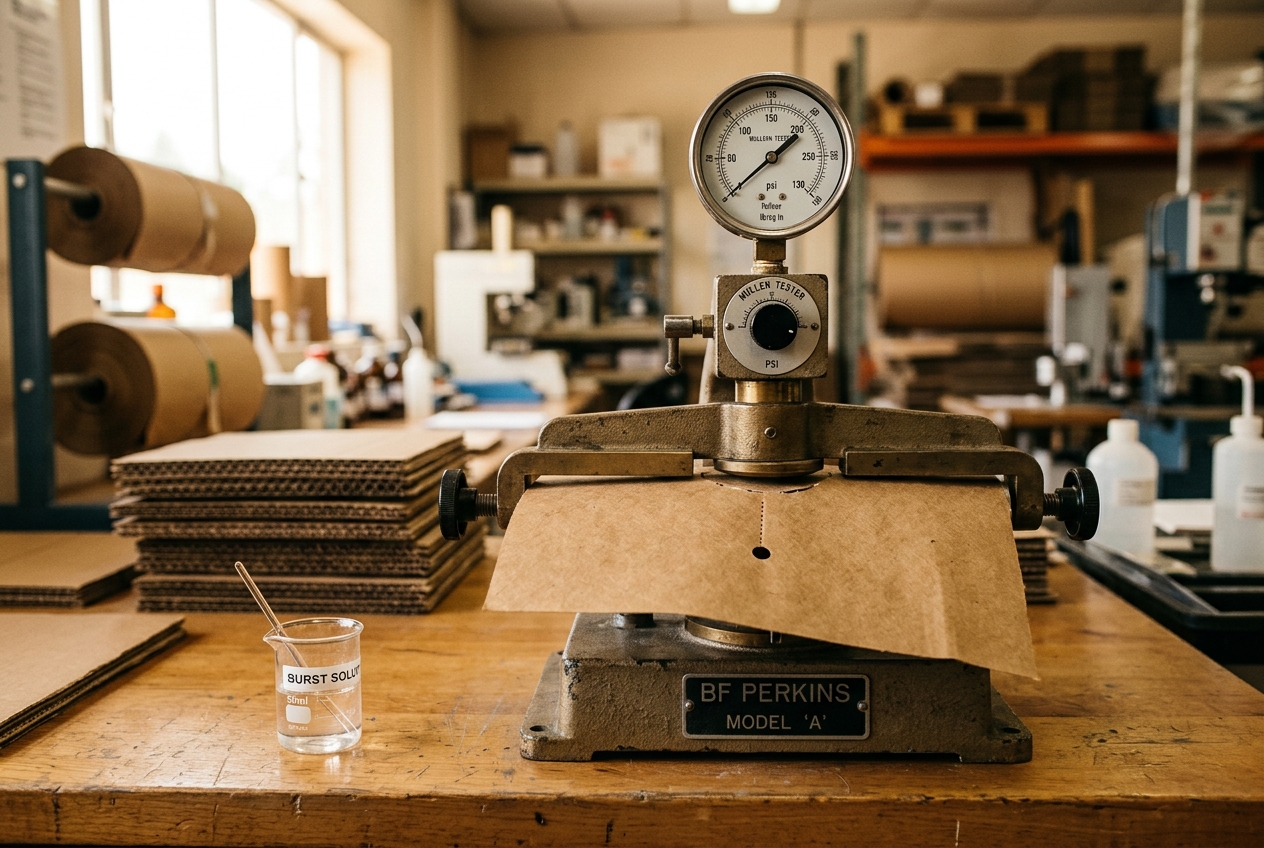
Burst Factor is the number every kraft and board buyer asks for first. A cationic base polymer dosed at the wet end (1.5–2 kg/tonne) improves wet-end chemistry, lifts BF by around 15% from the existing process condition and lets you cut starch consumption at the same time.
For kraft liner, sack kraft, corrugating medium and duplex board, Burst Factor (BF) is the specification that decides whether a reel is accepted or rejected. Mills usually chase BF with more refining, more starch or a better fibre mix – all of which cost money. A cationic base polymer dosed at the wet end is a simpler lever: it improves the wet-end chemistry itself, and BF follows.
What Burst Factor really measures
Burst Factor = Burst Strength (g/cm²) ÷ Grammage (gsm)
It normalises bursting strength to basis weight, so it tells you how well the fibres are bonded, not just how much fibre is in the sheet. Anything that increases inter-fibre bonding – better fines retention, more starch actually staying on the fibre, uniform formation – increases BF without adding grammage.
Why BF drops in real mill conditions
- Anionic trash from recycled fibre (OCC, mixed waste) neutralises the cationic starch and leaves it in the backwater
- Poor fines retention: fines carry most of the bonding surface area; when they wash out, bonding collapses
- High conductivity and ash blind the fibre surface and weaken hydrogen bonding
- Over-refining to compensate raises energy cost and slows drainage, so the sheet leaves the press wetter and weaker
The result is a mill that keeps adding starch and refining energy to hold a BF that still drifts from reel to reel.
How a cationic base polymer fixes the chemistry
The Burst Factor Booster is a cationic base polymer that is added in the wet end – typically at the machine chest or fan pump inlet where mixing is good. It works in three ways at once:
- Charge neutralisation – it neutralises anionic trash and dissolved colloidal substances, so cationic starch and other additives are free to bond to fibre instead of being lost to the backwater.
- Fines and filler retention – the polymer bridges fines to long fibre, keeping the high-surface-area material in the sheet where it creates bonds.
- Bond reinforcement – the polymer itself forms ionic bridges between anionic fibre surfaces, adding to the hydrogen bonding that starch provides.
Because the wet end becomes "cleaner" and more cationic-friendly, every kilo of starch you already dose works harder.
Results mills typically see
| Parameter | Existing process | With cationic BF booster |
|---|---|---|
| Burst Factor | Baseline | +15% from existing process condition |
| Starch consumption | Baseline | Reduced (same or higher BF with lower dosage) |
| Polymer dosage | – | 1.5–2.0 kg/tonne of paper |
| First-pass retention | Baseline | Improved |
| Backwater clarity | Cloudy, high COD | Clearer, lower load to ETP |
A 15% BF improvement from the existing process condition is the typical outcome when the polymer is dosed and tuned correctly – with no change to fibre mix or refining.
The starch saving
This is where the economics become obvious. Most kraft and board mills add 10–25 kg of starch per tonne to hold strength. With the polymer neutralising trash and improving retention, starch retention rises sharply, so mills either:
- Hold the same BF and cut starch dosage, or
- Keep the starch dosage and take the higher BF to move into a better-paying grade.
Either way the cost per tonne falls, and the reduced starch in the backwater also lowers BOD/COD at the effluent plant.
Dosing guidelines
- Dosage: 1.5–2.0 kg/tonne of paper (dry basis) – fine-tune with a mill trial
- Addition point: thick stock (machine chest) or fan pump inlet; ensure at least 30–60 seconds of mixing before the headbox
- Sequence: add the polymer before cationic starch so the trash is neutralised first
- Monitor: cationic demand / zeta potential, first-pass retention, backwater turbidity and, of course, BF at the reel
- pH: works across the normal 6.5–8.5 range; avoid dosing alongside strongly anionic additives at the same point
How to run a trial
- Record 3–5 days of baseline data: BF, RCT/CMT, starch kg/t, retention, backwater solids.
- Introduce the polymer at 1.5 kg/t and hold starch constant for 24 hours – watch BF rise.
- Step down starch in 10% increments until BF returns to the target; the gap is your saving.
- Fine-tune the polymer between 1.5 and 2.0 kg/t, lock in the dosage and add the polymer pump to the shift log.
Summary
Burst Factor is fundamentally a bonding problem, and bonding is a wet-end chemistry problem. A cationic base polymer dosed in the wet end cleans up the chemistry, lifts BF by around 15% from the existing process condition and reduces starch consumption – a rare case where quality goes up and cost goes down together.
VB Global supplies the Burst Factor Booster along with cationic starch, dry strength resin, retention aids and coagulants for kraft, corrugating medium and board mills. Ask our technical team to run a baseline survey and trial at your machine.